
Off-board component preparation
BGA reballing.Restore the array.
Define the ball map, alloy and package condition before rebuilding a BGA solder-ball array for its next SMT placement.
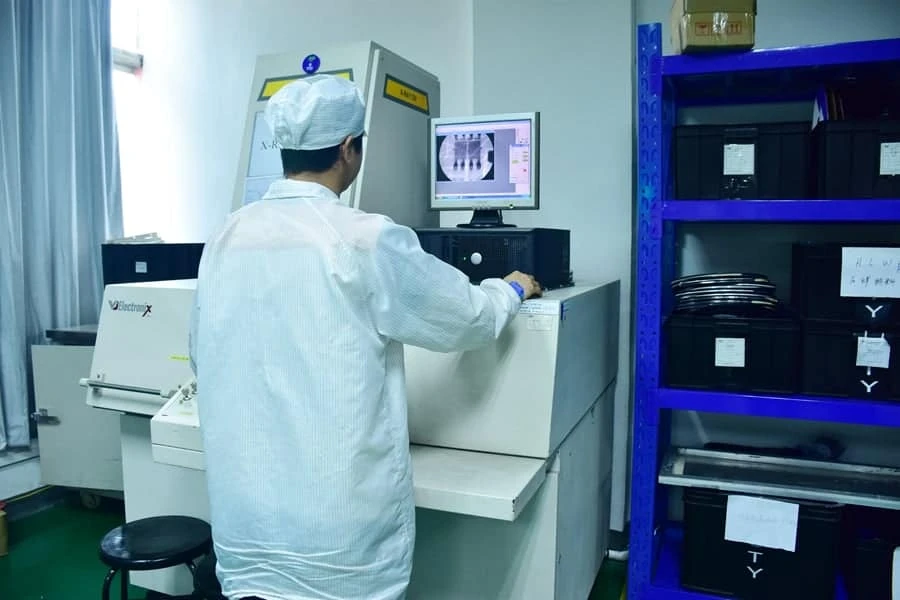
01 / Component scope
Start with an identifiable, acceptable package.
A controlled ball array before the SMT line.
BGA reballing is a component-preparation process performed before the package is assembled onto a PCB. It restores or creates a defined solder-ball array so the receiving SMT line can place the component with known alloy, geometry, cleanliness, and traceability.
This page is intentionally separate from BGA and QFN fine-pitch assembly. Reballing controls the off-board package; fine-pitch assembly controls paste printing, board placement, reflow, and inspection after the component reaches the PCB.
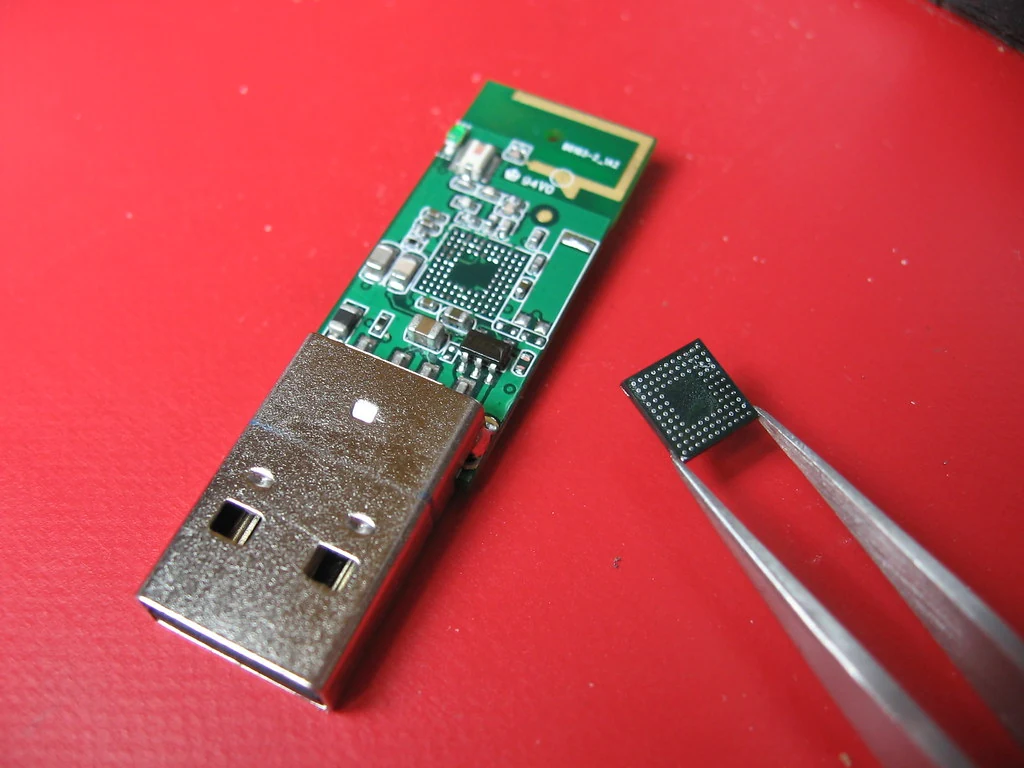
Start with the incoming package condition.
Choose the process from the incoming condition, not from the package name alone.
First ball placement
the package pads are prepared but do not yet have a solder-ball array.
Reballing
an existing array is removed or rejected and replaced with the required alloy and diameter.
Board-level BGA rework
the package is removed from an assembled PCB, the board site is repaired and cleaned, and the component is placed and validated on the board.
Replacement
use a new component when package damage, pad loss, delamination, contamination, or traceability risk makes reballing unsuitable.
02 / Incoming → Array placement
Qualify the package before placing the balls.
01
Incoming Package and Documentation Review
Work starts only after the physical package and the requested build condition agree.
• Confirm manufacturer part number, package drawing, ball map, pitch, orientation mark, quantity, and requested alloy.
• Inspect package edges, substrate, pads, warpage indicators, contamination, oxidation, and prior rework evidence.
• Record lot and date-code information when present; quarantine mixed or untraceable material for customer disposition.
• Confirm the moisture condition and whether bake or controlled dry handling is required before thermal processing.
• Confirm manufacturer part number, package drawing, ball map, pitch, orientation mark, quantity, and requested alloy.
• Inspect package edges, substrate, pads, warpage indicators, contamination, oxidation, and prior rework evidence.
• Record lot and date-code information when present; quarantine mixed or untraceable material for customer disposition.
• Confirm the moisture condition and whether bake or controlled dry handling is required before thermal processing.
02
Pad Conditioning Without Package Damage
Pad preparation must remove residual solder and contamination without thinning, lifting, or smearing the package pads. Flux chemistry, cleaning method, dwell time, and mechanical contact are selected for the package finish and prior condition.
Release to placement requires a complete pad array, a clean and wettable surface, no visible pad loss, and no package damage introduced during preparation. Components that fail this gate are held for disposition rather than pushed through reflow.
Release to placement requires a complete pad array, a clean and wettable surface, no visible pad loss, and no package damage introduced during preparation. Components that fail this gate are held for disposition rather than pushed through reflow.
03
Ball Map, Stencil, and Fixture Alignment
The stencil or placement fixture must match the package outline, pitch, ball map, and orientation. A diameter that fits the stencil is not enough: the finished ball geometry must also suit the pad diameter and the receiving assembly process.
• Verify package revision and orientation before loading.
• Confirm aperture or fixture compatibility with the specified ball diameter.
• Check that the package sits flat and cannot shift during distribution or transfer.
• Run an initial array check before the lot proceeds.
• Verify package revision and orientation before loading.
• Confirm aperture or fixture compatibility with the specified ball diameter.
• Check that the package sits flat and cannot shift during distribution or transfer.
• Run an initial array check before the lot proceeds.
04
Alloy and Solder-Ball Placement Control
Solder balls are controlled by alloy, nominal diameter, lot identity, and package location. Common review requests include SAC305, SAC405, Sn63Pb37, and alloy conversion. Ball diameter is confirmed against the package drawing, pad geometry, pitch, and fixture capability rather than selected from a generic range.
Before reflow, the array is checked for missing balls, doubles, mixed diameters, displaced balls, contamination, and incorrect orientation. Excess balls are removed from the work area so they cannot become foreign material in the next step.
Before reflow, the array is checked for missing balls, doubles, mixed diameters, displaced balls, contamination, and incorrect orientation. Excess balls are removed from the work area so they cannot become foreign material in the next step.
03 / Reflow → Protected lot
Release the array through four more gates.
05
Reflow Profile Matched to Alloy and Package
Reflow is not released by peak temperature alone. The profile must account for the specified alloy, package thermal mass, flux system, time above liquidus, ramp behavior, cooling, and the package supplier's temperature limit.
• Use a customer-approved or package-qualified profile when one is supplied.
• Record the applied recipe or profile reference for lot traceability.
• Prevent unnecessary repeat thermal cycles.
• Hold any package showing movement, incomplete wetting, collapse inconsistency, discoloration, or other abnormal response.
• Use a customer-approved or package-qualified profile when one is supplied.
• Record the applied recipe or profile reference for lot traceability.
• Prevent unnecessary repeat thermal cycles.
• Hold any package showing movement, incomplete wetting, collapse inconsistency, discoloration, or other abnormal response.
06
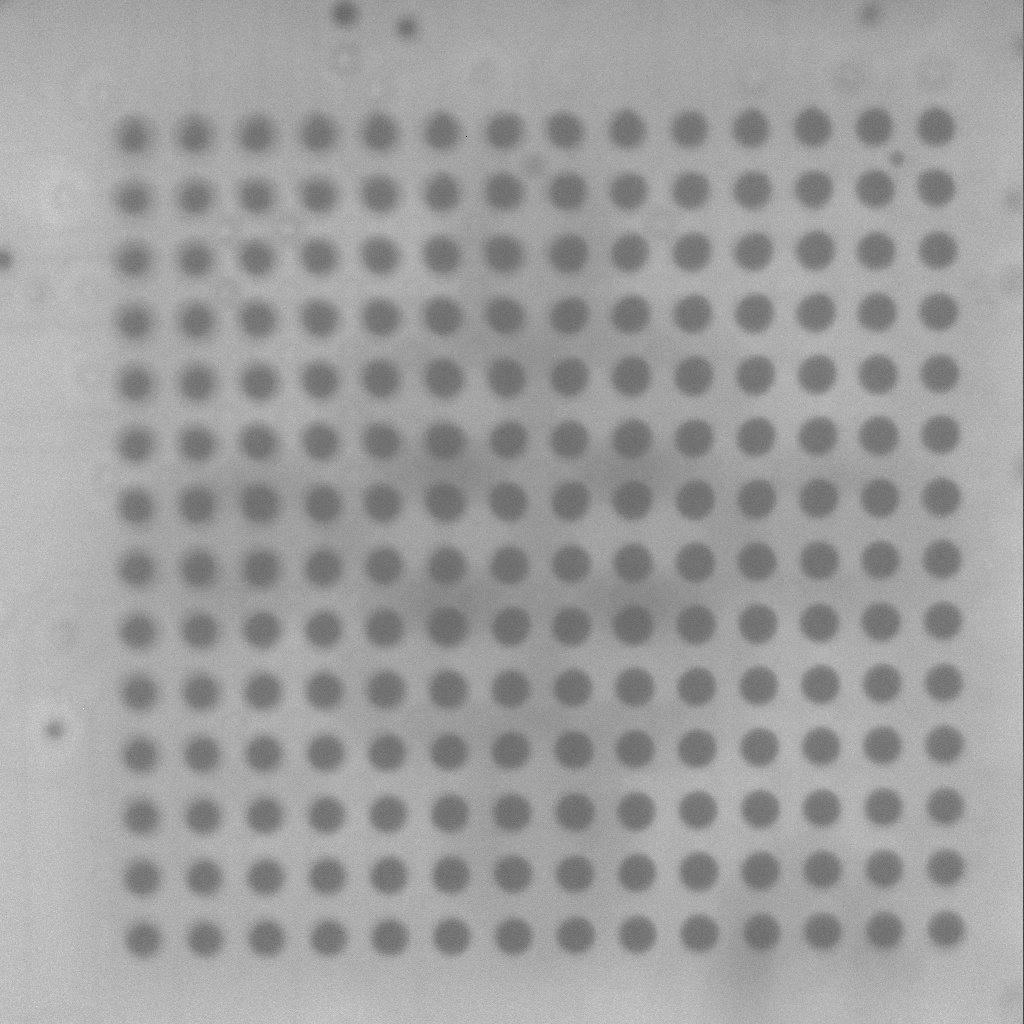
Optical and X-Ray Release Inspection
Post-reflow inspection answers three separate questions: is every required location populated, is the array aligned and geometrically consistent, and is there evidence of bridging or other hidden defects?
Optical and X-ray evidence does not by itself prove electrical function, internal die integrity, future solderability, or performance in the final assembly. Any electrical, dimensional, shear, alloy-verification, or sample-approval requirement must be defined in the RFQ and quotation.
• Optical inspection: package condition, orientation, peripheral alignment, ball shape, contamination, and handling damage.
• X-ray inspection: missing balls, doubles, gross geometry variation, bridging, and array-position anomalies.
• Ball-map reconciliation: populated and intentionally depopulated locations match the approved drawing.
• Customer evidence: inspection images or lot-level records are supplied when included in the quotation.
Optical and X-ray evidence does not by itself prove electrical function, internal die integrity, future solderability, or performance in the final assembly. Any electrical, dimensional, shear, alloy-verification, or sample-approval requirement must be defined in the RFQ and quotation.
• Optical inspection: package condition, orientation, peripheral alignment, ball shape, contamination, and handling damage.
• X-ray inspection: missing balls, doubles, gross geometry variation, bridging, and array-position anomalies.
• Ball-map reconciliation: populated and intentionally depopulated locations match the approved drawing.
• Customer evidence: inspection images or lot-level records are supplied when included in the quotation.
07
Cleaning and Residue Control
Cleaning is matched to the flux chemistry and package sensitivity. The objective is not merely a visually bright surface; it is a package free from loose debris, harmful residue, fingerprints, fibers, and cleaner entrapment before dry handling and packaging.
A final microscope check confirms array condition after cleaning. If the customer has an ionic-cleanliness or residue requirement, the method and acceptance criterion must be included in the RFQ because they are not interchangeable with visual inspection.
A final microscope check confirms array condition after cleaning. If the customer has an ionic-cleanliness or residue requirement, the method and acceptance criterion must be included in the RFQ because they are not interchangeable with visual inspection.
08
Packaging, Moisture Protection, and Traceability
Finished components are packaged for the next handling step, not for generic storage.
• Tape-and-reel: quote only after pocket fit, orientation, cover-tape condition, and receiving-line requirements are defined.
• Customer-specified tray: confirm the exact tray format and restraint needed to protect the package in transport and handling.
• Moisture protection: use dry packaging, desiccant, and labels when the package condition or customer specification requires it.
• Traceability label: identify part number, quantity, lot or date code, alloy, ball diameter, and processing lot as agreed.
• Tape-and-reel: quote only after pocket fit, orientation, cover-tape condition, and receiving-line requirements are defined.
• Customer-specified tray: confirm the exact tray format and restraint needed to protect the package in transport and handling.
• Moisture protection: use dry packaging, desiccant, and labels when the package condition or customer specification requires it.
• Traceability label: identify part number, quantity, lot or date code, alloy, ball diameter, and processing lot as agreed.
04 / Hold & disposition
Stop when the risk exceeds the agreed boundary.
Reball, rework or replace?
Reballing is appropriate when the package body and pads are acceptable, the required ball map and materials are known, and the component's identity and thermal history can be controlled. It is not an automatic repair for every failed BGA.
Reball the component
when the off-board ball array is missing, damaged, contaminated, or must change to an approved alloy.
Use board-level rework
when the defect is at the assembled PCB site and board pads, placement, and assembly inspection must be controlled together.
Replace the component
when pad loss, package cracking, delamination, uncontrolled moisture exposure, repeated thermal cycles, or traceability gaps exceed the approved risk boundary.
Run engineering review
when package drawings, ball maps, alloy requirements, or acceptance criteria conflict.
Acceptance belongs at each gate.
Release Gates, Failure Modes, and Reference Practices
Typical failure modes include pad loss during preparation, mixed alloy, wrong ball diameter, missing or doubled balls, array shift, bridging, incomplete wetting, residue, moisture exposure, package damage, and loss of lot traceability. Each risk is assigned to an incoming, in-process, or final release gate rather than left to a single end inspection.
Reference practices may include IPC-7095E for BGA design, assembly, inspection, repair, and reliability guidance, and IPC/JEDEC J-STD-033D for handling, packing, shipping, and use of moisture/reflow-sensitive devices. Neither replaces the purchase order, package-supplier limits, customer drawing, or agreed acceptance criteria.
Reference practices may include IPC-7095E for BGA design, assembly, inspection, repair, and reliability guidance, and IPC/JEDEC J-STD-033D for handling, packing, shipping, and use of moisture/reflow-sensitive devices. Neither replaces the purchase order, package-supplier limits, customer drawing, or agreed acceptance criteria.
05 / Receiving handoff
Define the deliverable and the data needed to quote it.
Evidence for the receiving assembler.
The useful deliverable is a released component lot with enough evidence for the receiving assembler to understand what was changed.
| Deliverable | Record to agree |
|---|---|
| Incoming condition | Incoming material and package-condition record. |
| Array definition | Approved ball map, alloy, diameter, and orientation reference. |
| Process traveler | Process traveler with preparation, placement, reflow, cleaning, and packaging steps. |
| Inspection evidence | Optical or X-ray inspection evidence when specified. |
| Disposition | Nonconformance and disposition record for held or rejected components. |
| Packaging & identification | Final packaging and traceability label matched to the customer's receiving format. |
Scroll the table to review all columns.
Define the incoming lot and the released array.
Send the package data below so feasibility, tooling, inspection, packaging, and quotation are based on the same build definition.
| RFQ item | Package data to supply |
|---|---|
| Package drawing | Manufacturer part number, package drawing, ball map, pitch, dimensions, and orientation mark. |
| Incoming lot | Quantity, lot and date codes, incoming condition, prior rework history, and moisture status. |
| Alloy & diameter | Required solder-ball alloy and nominal diameter; identify whether alloy conversion is requested. |
| Thermal limits | Customer or package-supplier reflow limits and any approved profile. |
| Release evidence | Required optical, X-ray, cleanliness, dimensional, or traceability records. |
| Packaging | Packaging format, orientation, labeling, dry-pack, and receiving-line requirements. |
| Acceptance & delivery | Acceptance criteria, sample approval requirement, delivery lot split, and disposition rules for rejects. |
Scroll the table to review all columns.
PRACTICAL QUESTIONS
Before you release the work.
What is the difference between BGA reballing and board-level BGA rework?
Reballing prepares an off-board BGA package by replacing or adding solder balls. Board-level rework removes and reinstalls a package on an assembled PCB and also requires board-pad inspection, site preparation, placement, and assembly-level validation.
Which BGA package data is required for quotation?
Provide the manufacturer part number, package drawing or ball map, package quantity, ball diameter, alloy, pitch, moisture condition, incoming state, packaging requirement, and requested inspection or release records.
Which solder-ball alloys and diameters can be reviewed?
Common requests include SAC305, SAC405, Sn63Pb37, and alloy conversion. Ball diameter is reviewed against the package drawing, pad geometry, pitch, stencil or fixture availability, and customer acceptance criteria rather than promised as a generic range.
How is a reballed BGA released?
Release can include ball-count and ball-map verification, optical checks for alignment and geometry, X-ray review for missing balls or bridging, cleanliness review, lot traceability, and customer-specified inspection records.
How are finished BGA components packaged?
Packaging is quoted for the receiving SMT process and package format. Options can include customer-specified trays or tape-and-reel, plus dry packaging, desiccant, and traceability labels when moisture protection is required.
What does PCB rework cover?
PCB rework can include component removal, site preparation and replacement followed by inspection and testing. Reballing applies to a suitable reusable BGA package only after its condition and the approved rework process are reviewed.
How does underfill affect BGA rework?
Cured underfill can make component removal destructive or impractical. Review the resin, board and package condition, thermal limits and approved repair method before deciding whether rework is feasible.
ENGINEERING & PRODUCTION REVIEW
Review the incoming BGA lot.
Send the package definition and the condition in which it will arrive.
- Part number, package drawing and ball map
- Quantity, lot history and moisture condition
- Required alloy, ball diameter and thermal limits
- Inspection records and receiving packaging