SMT print control

Control the print.Before placement.

Solder paste inspection links measured deposits to printer adjustments before components and reflow add complexity.

SPI scope
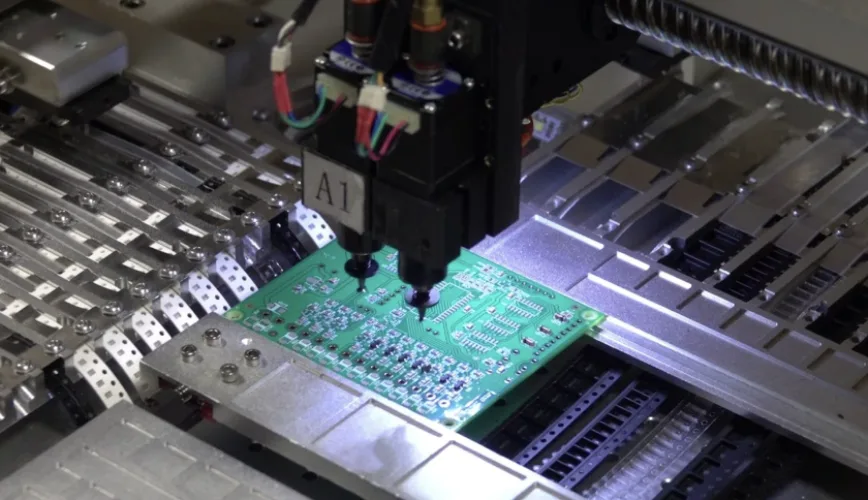
SMT placement equipment working above a circuit board

01 / Printed deposits

Measure the paste before components cover the pads.

APTPCB is a PCB manufacturing and PCB assembly factory, focused on delivering stable, repeatable quality for your electronic products. As part of our PCBA Quality & Testing process, we use Solder Paste Inspection (SPI) on the SMT line to control one of the most critical steps in assembly: solder paste printing.
SPI is not a separate service we sell on its own. It is built into our SMT production to help you get higher yields, more reliable joints, and fewer hidden defects from the very first print.
Solder Paste Inspection (SPI) checks how much solder paste has been printed on each pad, and where it has been printed, before any components are placed. On every PCB panel, SPI measures things like paste volume on each pad, paste height and area, offset/misalignment versus pad position, bridging or excessive paste between pads, and insufficient or missing paste in critical areas.

02 / The SMT print gate

Inspect the print, correct the process, then place.

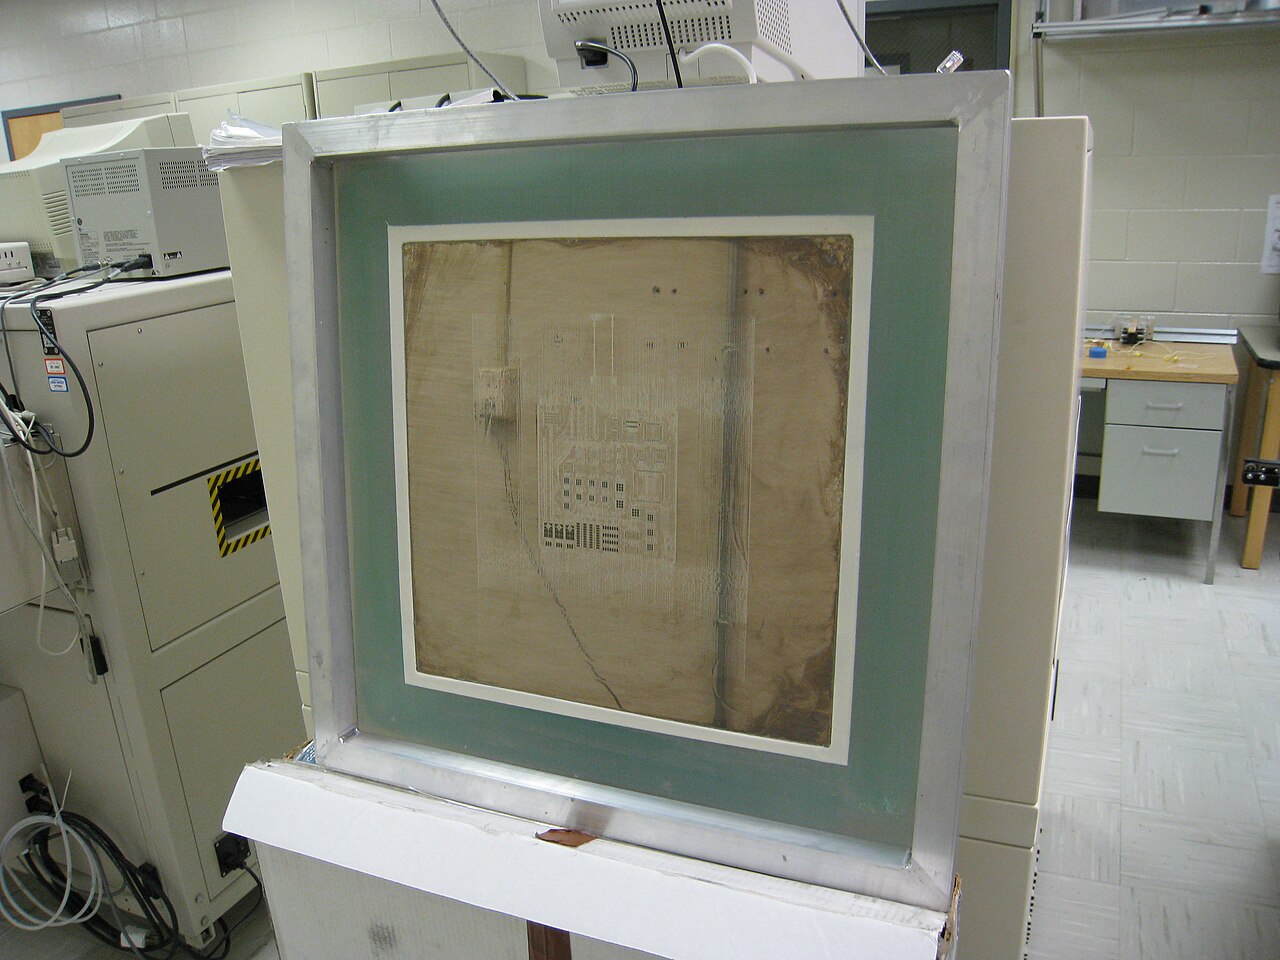
The stencil defines the printed deposits. SPI feeds the print decision before placement and reflow make correction more difficult.

Metal solder-paste stencil mounted in a rectangular frame
On our SMT lines, Solder Paste Inspection is integrated directly after the solder paste printer and before placement:

Step 1

Solder paste printing onto PCB pads using a stencil

Step 2

Solder Paste Inspection (SPI) checks paste volume, height, and alignment

Step 3

If needed, the line can be stopped or adjusted (stencil cleaning, print alignment, pressure, etc.)

Step 4

Only boards that pass SPI move on to component placement and reflow soldering

03 / Deposit & trend

Read volume, height, alignment and drift together.

Our SPI process is configured around your design and risk level. Typical checks include:

Paste Volume & Height:

  • Overall paste volume per pad
  • Paste height consistency across the board
  • Monitoring of critical nets and fine-pitch components

Too little paste can cause opens or weak joints; too much can cause bridging and voids. SPI keeps this under control.

Paste Alignment:

  • Lateral offset relative to pad centers
  • Skew or smear on small pads (e.g. 0402, 0201)
  • Misalignment trends across the panel (print shift)

If we detect systematic offset, we adjust printer alignment, stencil cleaning, or pressure.

Defects & Trend Monitoring:

  • Local or global insufficient paste
  • Excess paste and bridging risk
  • Missing paste in specific areas
  • Printing defects over time (e.g. stencil wear, contamination)

Data from SPI is used not only to accept/reject boards, but to fine-tune the process.

04 / Measurement recipe

Match the inspection settings to pad and package risk.

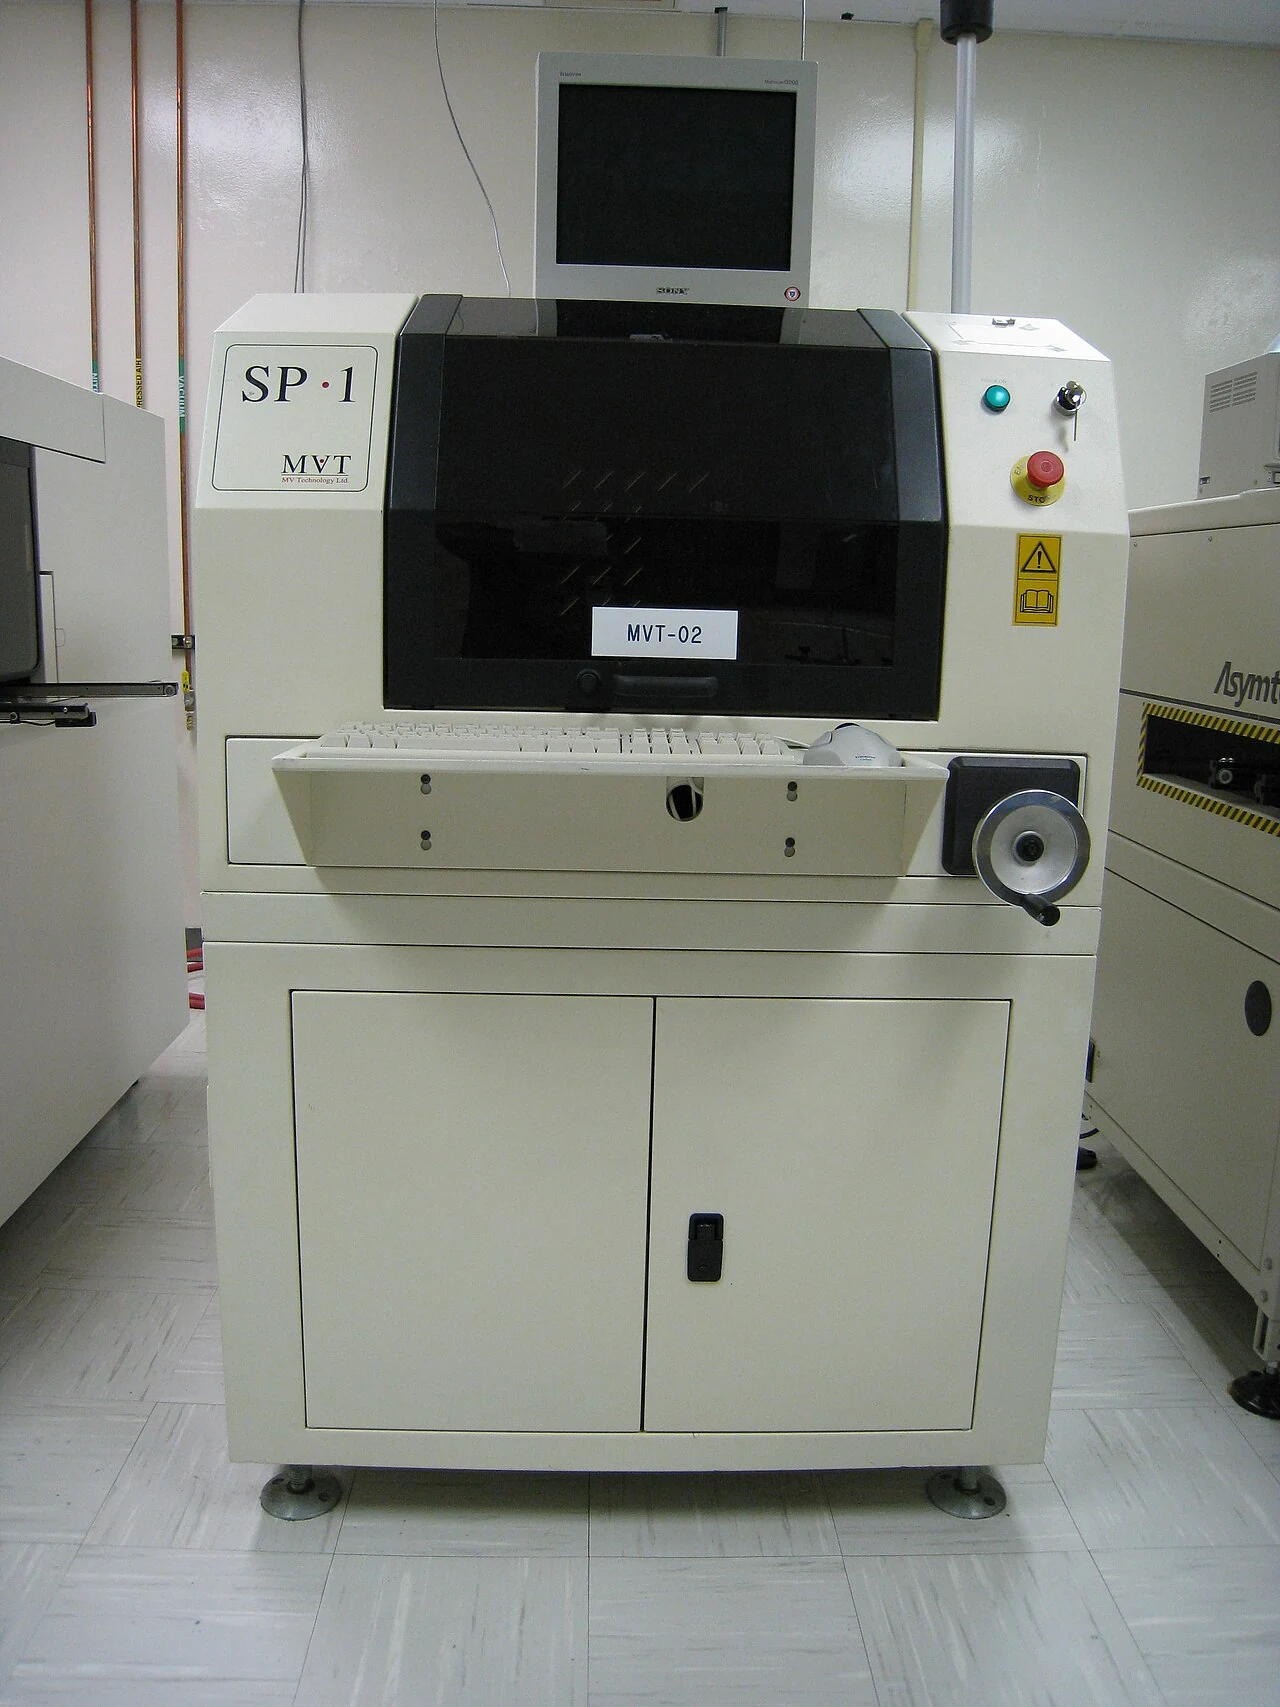
Solder paste inspection equipment with a conveyor and measurement enclosure.
For modern, high-density PCB assemblies, 3D SPI brings added control:
We use 3D SPI especially on boards with:
For simpler or lower-risk boards, we may use lighter SPI settings aligned with your cost and speed needs.
3D SPI measurementPackage & risk considerations
Measures true 3D paste volume instead of just 2D area

Detects subtle height variations that affect BGA and fine-pitch joints

Gives more accurate feedback when optimizing stencil design and printing parameters
BGA and µBGA packages

QFN / LGA and other bottom-terminated components

Fine-pitch ICs and 0.4 mm devices

High-reliability applications where joint quality is critical

Scroll the table to review all columns.

05 / Production context

Carry print feedback into dense and repeat builds.

Our Solder Paste Inspection is particularly valuable for:
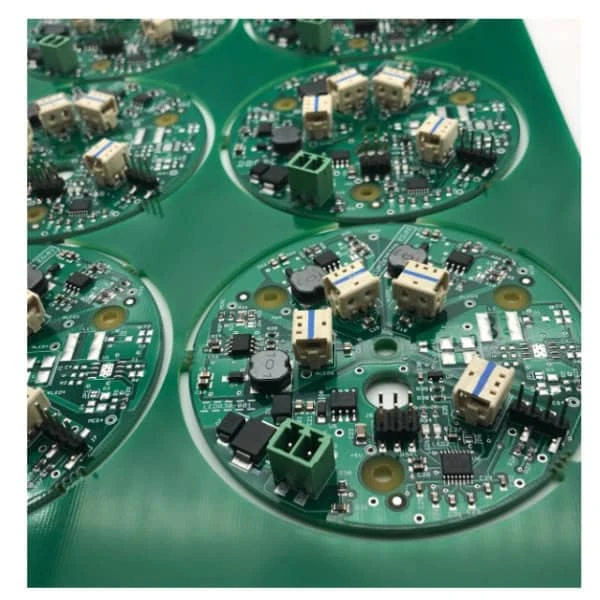
Circular populated circuit boards with surface-mount parts and connectors
Compact assemblies bring package pitch and deposit consistency into the print review.

High-Density Designs

Fine-pitch, BGA-heavy layouts where paste volume and position are critical for yield.

Consumer Electronics

Wearables, smartphones, and compact devices requiring consistent, reliable solder joints.

Industrial Control

Automation and control boards where reliability and repeatability are essential.

Power Electronics

Power supplies and converters where thermal paths and joint integrity matter.

Telecom & Networking

High-speed communication equipment with complex, dense PCB layouts.

Medical Devices

Healthcare electronics requiring strict quality control and traceability.

Production context and repeat-build feedback

When SPI Is Especially Important


High-density consumer electronics and wearables

Industrial control and automation boards

Power electronics where joint reliability and thermal paths matter

Telecom and networking hardware with fine-pitch and BGA-heavy layouts

Any design where you care about reliability, repeatability, and yield


If your design pushes limits on pad size, pitch, or component density, SPI is one of the reasons your boards can still be built consistently and safely.

Benefits of SPI for Your Project

Because SPI is fully integrated into our PCB assembly process, it directly raises your overall assembly yield. By detecting issues like insufficient, excessive, or misaligned solder paste before components are placed, we prevent many solder-related defects from ever reaching AOI, X-ray, or functional test. That means fewer opens, shorts, and weak joints, as well as significantly less rework and scrap—especially important for fine-pitch, high-density, or BGA-heavy designs where paste volume and position are critical.

SPI also helps stabilize quality over time and across repeat orders. With real-time feedback from the SPI system, we can continuously control and fine-tune the printing process, maintaining consistent results from batch to batch. The inspection data allows us to optimize stencil and pad design, adjust print parameters, and, when useful, share insights with you for future design improvements. The result is more predictable performance, smoother production, and lower risk when you move to smaller packages or more complex layouts.

06 / The wider inspection chain

Keep the later solder-joint and electrical checks.

Solder Paste Inspection is one part of a layered PCBA quality system at APTPCB. Alongside SPI, we also use:
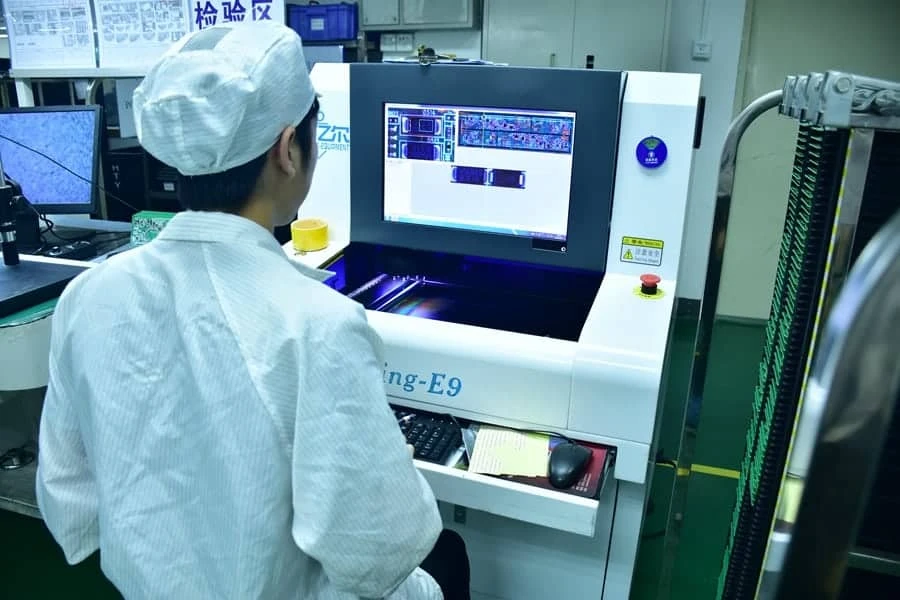
Operator reviewing a populated circuit board at an automated optical inspection station
Optical inspection reviews visible placement and solder-joint features.
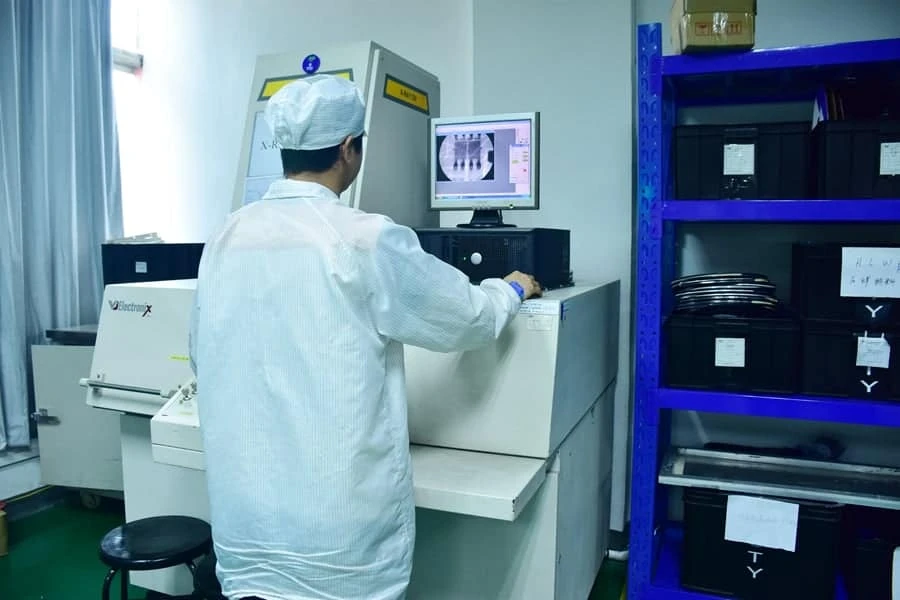
Operator viewing circuit board X-ray images at an inspection workstation
X-ray inspection requires a defined viewing method, target feature and acceptance rule.
Quality gateWhat it checks
AOI (Automated Optical Inspection)– after placement and reflow
X-ray inspection– for hidden joints (e.g. BGA, bottom-terminated packages)
In-Circuit Test (ICT)– for electrical verification where applicable
Functional Test (FCT)– to confirm the complete board works as intended

Scroll the table to review all columns.

SPI controls solder paste at the start; AOI/X-ray/ICT/FCT confirm solder joints and functionality at the end. Together, they make your PCBAs much more reliable.

ENGINEERING REFERENCE

Additional SPI benefits and integrated assembly context

Why Solder Paste Inspection Matters for Your PCBA
Solder paste printing is often the single biggest source of SMT defects. If it's wrong at the stencil stage, everything afterwards is just 'fixed' on top of a bad foundation.
By catching printing problems immediately, we prevent downstream defects such as open solder joints, bridges and shorts, head-in-pillow defects, and weak or marginal connections.
Using SPI as part of our PCBA process helps you:
Improve first-pass yield on assembled boards
Reduce rework and scrap from shorts and opens
Stabilize quality between different batches and builds
Support fine-pitch, BGA, and high-density designs where paste volume is critical
For dense, miniaturized, or reliability-focused assemblies, SPI is a key reason your boards pass functional test and survive in the field.
Work with APTPCB for PCB Assembly with SPI Built In
APTPCB is not just a test provider—we are a PCB manufacturing and PCB assembly factory with SPI, AOI, X-ray, ICT, and Functional Test integrated into our PCBA production lines.
When you place PCB assembly orders with us, Solder Paste Inspection is part of the process, helping us:
Print solder paste correctly
Build reliable joints
Deliver PCBAs that meet your electrical and functional expectations
If you are planning a new project or migrating an existing design and want a partner that takes PCBA Quality & Testing – including Solder Paste Inspection – seriously, we're ready to help.

PRACTICAL QUESTIONS

Scope, acceptance and practical limits

What does solder paste inspection measure?
Solder paste inspection measures printed paste features such as volume, height, area and position before component placement. Its recipe and acceptance limits must match the stencil, pads and assembly process.

ENGINEERING & PRODUCTION REVIEW

Plan print control for your assembly.

Identify the package and pad features that need attention in the SMT inspection plan.

  • PCB data and assembly revision
  • BOM and fine-pitch / bottom-terminated packages
  • Stencil or paste requirements if specified
  • Acceptance criteria and required records