Material receipt → production release

Received is a status.Released is a decision.

Link incoming material to the approved BOM, handling requirements and documented lot disposition before assembly.
Sampling & disposition
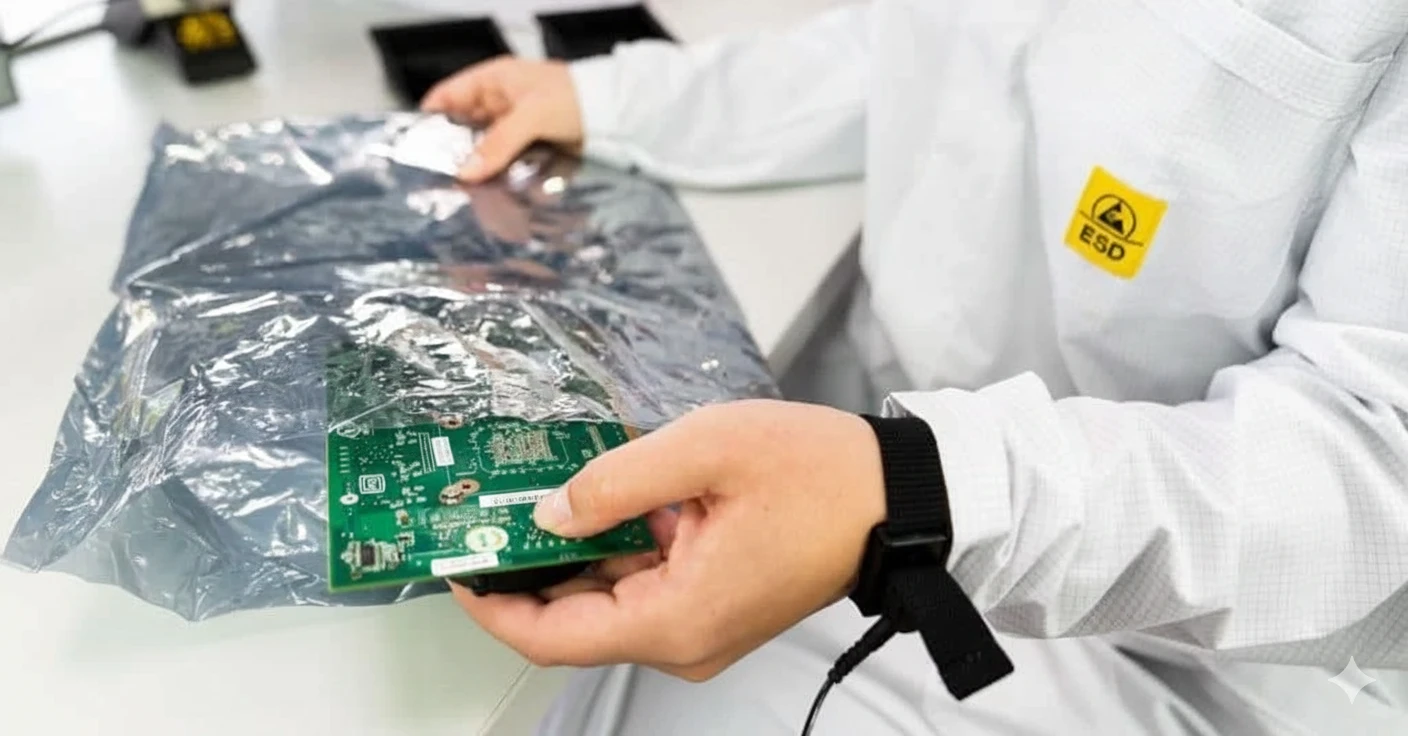
ESD-protected handling of a circuit board beside an antistatic bag
ESD-protected handling is one part of material control from receipt to kitting.

01 / Release status

Give each incoming lot a traceable disposition.

A sampling plan is not a fixed property of the supplier. Inspection level, sample size and acceptance rule depend on the contract, component risk, supply route, lot history and customer requirements. If ISO 2859-1:2026 is used, the AQL, inspection level and lot rules must be defined in advance.
The result should be unambiguous: released, on hold, pending additional inspection or submitted for customer disposition. Buyers benefit less from a long checklist than from a traceable link between risk, inspection, finding and release.
DispositionRelease condition
ReleasedThe received lot meets the agreed inspection and acceptance criteria.
On holdUnresolved identity, condition or source issues prevent production release.
Additional inspectionThe risk requires a suitable, separately agreed inspection method.
Customer dispositionA documented customer decision resolves a discrepancy before assembly.

Scroll the table to review all columns.

02 / Material risk

Check the received lot against its intended build.

What PCBA incoming quality control resolves before assembly
Incoming quality control (IQC) is the release gate between material receipt and production. It does more than confirm that the ordered quantity arrived: it checks whether the actual lot matches the approved BOM revision, intended package and agreed storage and traceability rules.
IQC complements component sourcing and final PCBA inspection. It cannot prevent every downstream defect, but it reduces the chance that wrong, damaged, moisture-exposed or unresolved material reaches kitting, SMT or through-hole assembly.
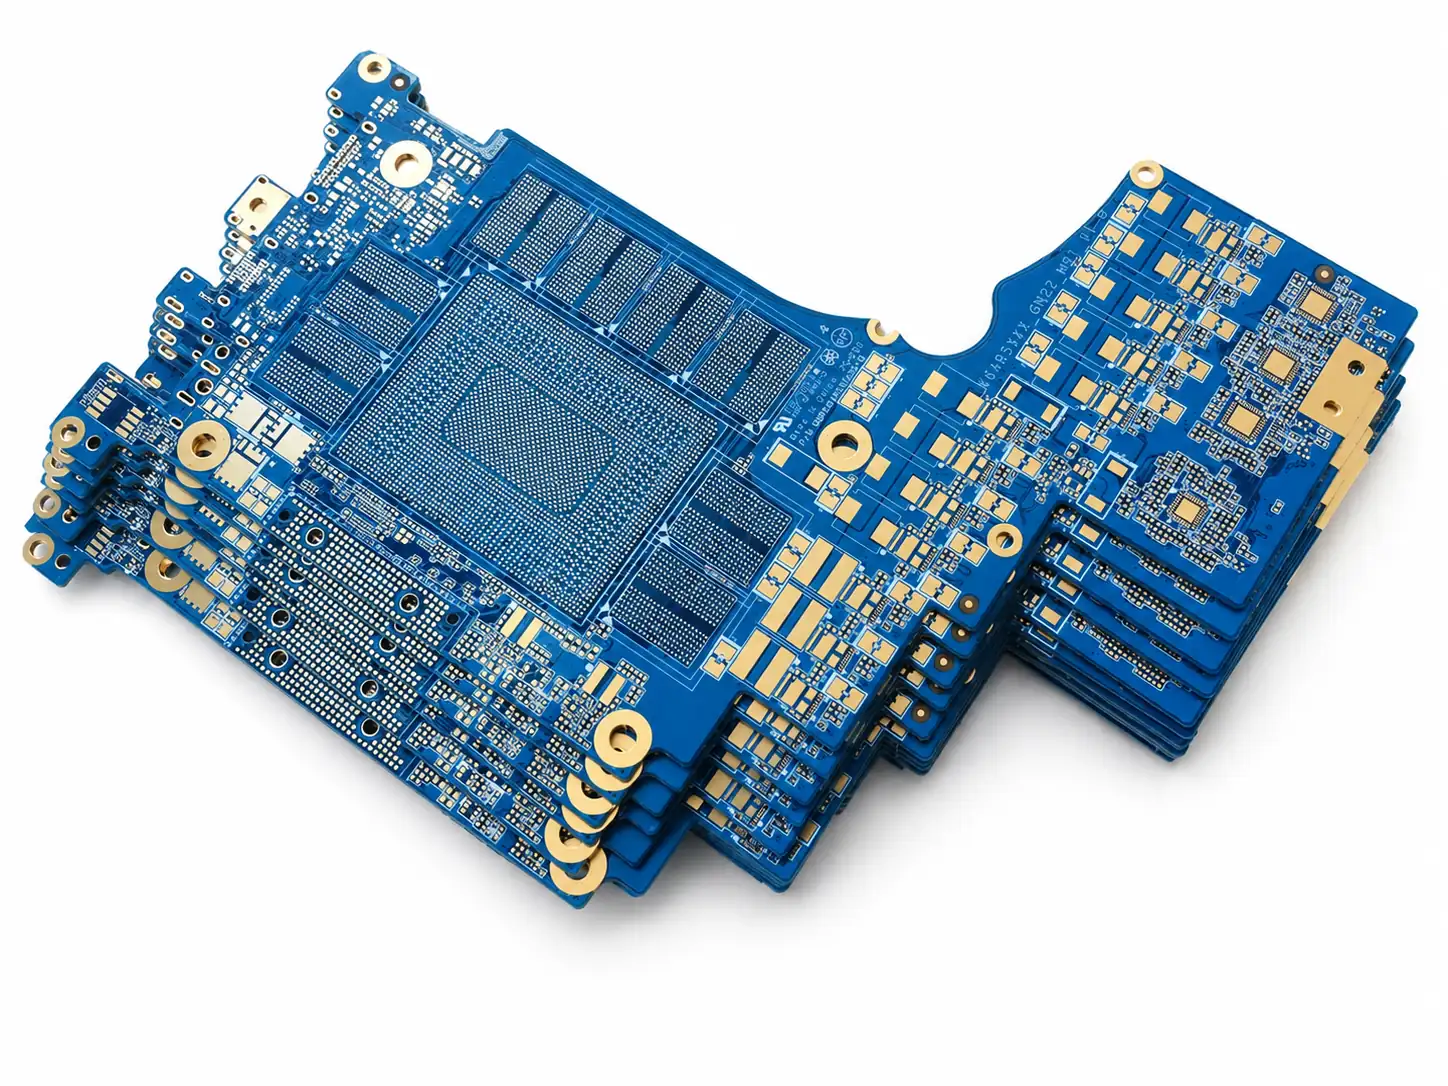
Blue bare circuit boards with component footprints and plated holes
Incoming bare boards can be checked against released fabrication requirements.

Risk-based IQC release matrix for component lots

RiskInspection pointCustomer data neededPossible release evidence
BOM or AVL mismatchCheck manufacturer part number, manufacturer, package, value, tolerance, voltage, temperature range, polarity and approved alternates.BOM revision, AVL, do-not-substitute lines, approved alternates and change status.Deviation record, documented alternate approval or hold decision.
Unclear source or counterfeit riskReview supply channel, labels, packaging condition, date and lot codes, surface markings and visible relabeling signs.Source restrictions, CoC/CoA needs, critical-parts list and contractual test requirements.Supplier trace, label photographs, quarantine decision and, where applicable, an external laboratory report.
Moisture-sensitive SMDsCheck MSL label, moisture-barrier bag, humidity indicator card, desiccant, opening time and remaining floor life.MSL level, package, process instruction and dry-storage or bake rules.Material status, opening-time record and documented kitting release.
Customer-supplied componentsCheck packing list, project assignment, quantity, labels, packaging, visual condition and agreed ESD/MSL data.Packing list, owner/project ID, shortage rule and disposition for excess or rejected material.Receiving report, discrepancy notice, lot link and customer disposition.
Critical, obsolete or high-cost partsIncrease inspection depth according to function, availability, source, lot history and failure consequence.Criticality, date-code window, traceability depth, test method and retention period.Inspection summary, sampling data, retained labels or a nonconformance report.

Scroll the table to review all columns.

Inspection scope, sampling and release evidence are agreed by project before the material is used.

03 / The approved BOM

Resolve the part and revision before kitting.

Receiving connects the actual component lot to its approved manufacturer part number, package and permitted alternates.
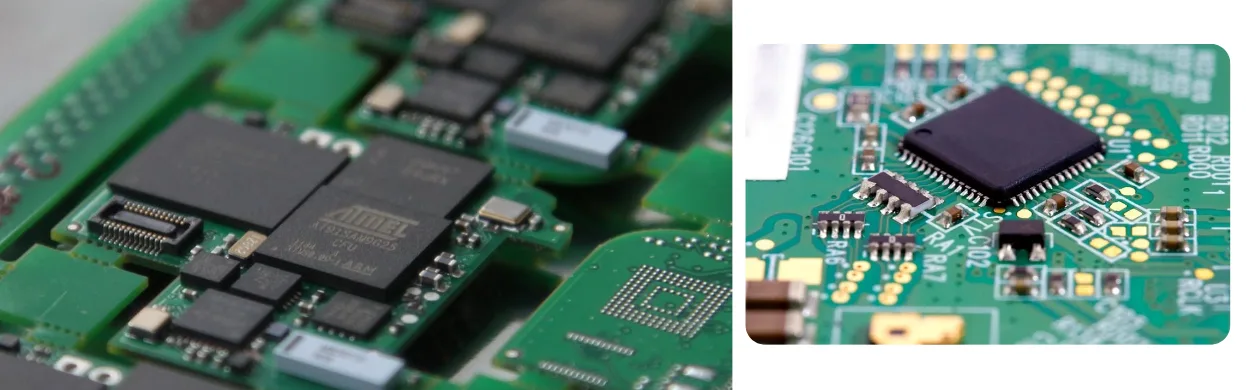
Close-up views of integrated circuit packages and small components on populated boards
The inspection baseline should identify every critical BOM line by manufacturer part number, manufacturer, package, electrical limits, temperature grade, polarity and permitted alternates. A mismatch, EOL status or allocation becomes a decision point; an alternate enters the production revision only after documented customer approval.
For repeat builds, revision, approval date and decision history matter as much as the component value. They show which lot entered each assembly revision and why a deviation was accepted or rejected.

04 / Inspection boundaries

Define when receiving checks need additional evidence.

Scope note Label and visual checks can reveal anomalies. Additional tests require a suitable technical plan and an agreed disposition before material release.
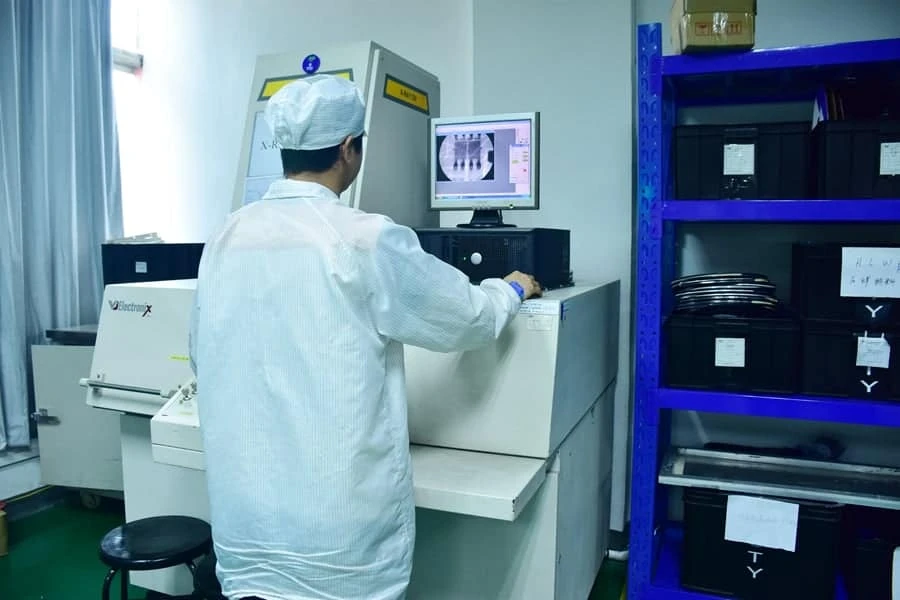
Operator viewing circuit board X-ray images at an inspection workstation
X-ray inspection requires a defined viewing method, target feature and acceptance rule.

Baseline receiving inspection

Baseline IQC can cover documents, labels, packaging, quantity, visible damage, MSL status and traceability data. These checks provide a practical release basis, but they are not standalone proof of authenticity for semiconductors or other counterfeit-risk parts.

Special testing & authenticity review

Higher-risk material remains on hold until inspection depth and disposition are defined. Additional methods such as X-ray, X-ray fluorescence, decapsulation, electrical characterization or external laboratory testing are included only when technically suitable, available and agreed in advance. SAE AS5553 or IEC 62668-1:2019 + AMD1:2024 applies only when the contract, industry or customer requires that level of control.

05 / Handling status

Carry moisture and ESD requirements through kitting.

Moisture and electrostatic risk start before the SMT line. For moisture-sensitive devices, the MSL label, moisture-barrier bag, humidity indicator card, desiccant, opening time and remaining floor life should be recorded before release. Baking or dry storage follows the component requirement and the agreed process rule.
Relevant technical references include IPC/JEDEC J-STD-033D for handling, packing, shipping and use of moisture/reflow-sensitive devices; J-STD-020F for MSL classification; and IEC 61340-5-1:2024 for protection of electronic devices from electrostatic phenomena. The implementation must fit the component and project.

06 / Consigned material

Keep project ownership and discrepancies visible.
Customer-supplied components can enter the same project release flow. The inputs are a clear packing list, owner and project assignment, expected quantity, part identity, and rules for shortages, excess material and discrepancies.
Label, packaging, quantity, visual condition and MSL/ESD differences should be resolved before assembly. This gives the customer a clear disposition point before an unresolved lot consumes production time or puts assembled boards at risk.
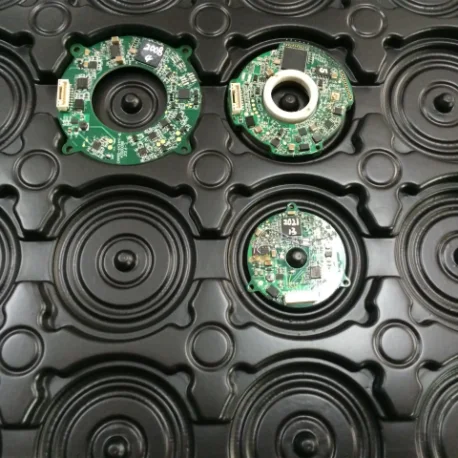
Circular electronic assemblies held in individual recesses of a black protective tray
Sample identity and protective handling remain relevant through inspection and handover.

Inputs that shorten IQC planning

For quotation and inspection planning, send the BOM, AVL and date-code limits, do-not-substitute lines, approved alternates, consigned-parts list, MSL requirements, required supplier evidence, sampling rule, quarantine and release conditions, and required traceability depth.

APTPCB will confirm which baseline checks can be covered within the PCBA project, which special tests need separate confirmation and which records are proposed as release evidence.

PRACTICAL QUESTIONS

Scope, acceptance and practical limits

What does incoming quality control cover for a PCBA build?
The agreed IQC scope can cover identity, quantity, label, packaging and visual checks plus verification against the BOM, AVL, date and lot codes, and MSL/ESD requirements. The lot is then released, blocked or presented for disposition.
What information does APTPCB need for an IQC plan?
Provide at least the BOM and revision, manufacturer part numbers, AVL or approved alternates, do-not-substitute lines, date-code limits, MSL requirements, a consigned-parts list, and the required acceptance evidence or criteria.
Does visual inspection prove that an electronic component is authentic?
No. Label, packaging and traceability checks can reveal anomalies, but they do not replace comprehensive authenticity testing. Higher-risk lots need a separate plan using suitable internal or external methods before release.
How is the IQC sample size determined?
Sampling depends on the contract, component risk, supply source, lot history and customer requirements. If ISO 2859-1:2026 or a customer plan applies, the inspection level, AQL and acceptance rule must be set before production release.
How are moisture-sensitive SMD components controlled?
The plan can record the MSL label, moisture-barrier bag, humidity indicator card, desiccant, opening time and remaining floor life. Baking or dry storage is applied only under the component requirement and the agreed process rule.
Can customer-supplied components be included in the IQC process?
Yes. Consigned components can enter the project IQC plan with a packing list, project assignment, quantity reconciliation, label and visual checks, and the agreed MSL/ESD and traceability data. Discrepancies are presented for disposition before assembly.

ENGINEERING & PRODUCTION REVIEW

Define the incoming material release gate.

Identify the material risks, permitted alternates and records needed for your PCBA project.

  • BOM revision, AVL and approved alternates
  • Date-code limits and source restrictions
  • MSL / ESD and consigned-parts requirements
  • Sampling, release criteria and required evidence